You know the seal is generating heat — but how much? That number drives every downstream decision: flush flow rate, cooler sizing, barrier fluid selection, and whether a Plan 11 is sufficient or you need to step up to a Plan 53B. Yet most published references either present the formula without a worked example or confuse face-generated heat with heat soak from the pump casing. These are two different heat sources requiring two different calculations.
The face-generated heat formula gives you the answer: Q = f x Pf x V x A. Each variable is measurable or available from the seal drawing, and a complete worked example on a 2-inch seal at 3600 RPM shows how the numbers come together.
What Generates Heat at Mechanical Seal Faces
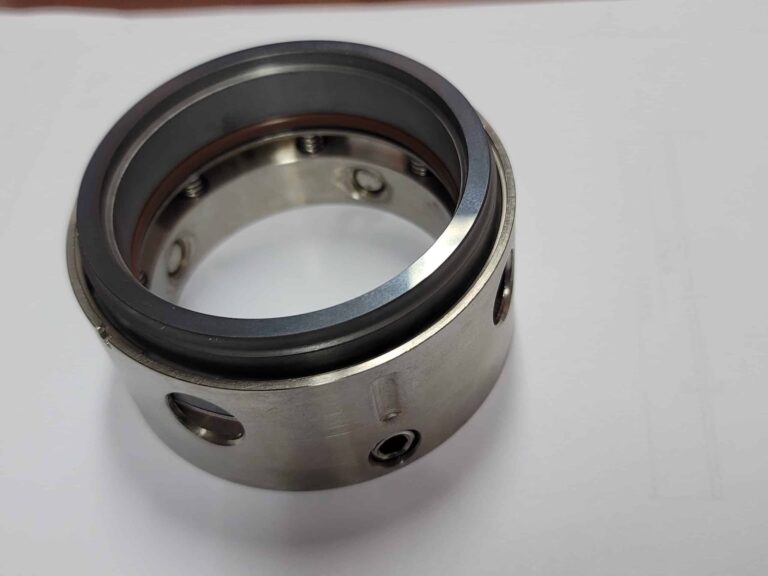
Seal faces generate heat through two mechanisms: rubbing friction between the contact surfaces and viscous shearing of the fluid film between them. Rubbing friction dominates in most applications and accounts for the majority of the thermal load.
Rubbing Friction
When two seal faces press together and rotate, the friction between them converts mechanical energy directly into heat. This is a power loss — energy that was supposed to move fluid is instead warming up the seal chamber. The heat generated scales with four variables: friction coefficient, face pressure, sliding velocity, and contact area. Increase any one, and heat rises proportionally.
The friction coefficient between dissimilar face materials typically ranges from 0.02 to 0.08 for well-lubricated seal faces, though values from 0.01 to 0.3 appear across the full range of operating conditions. A carbon graphite ring running against tungsten carbide or silicon carbide in clean water service sits around 0.07 — that is the value I use for most standard calculations until I have test data saying otherwise.
Viscous shear adds a secondary heat contribution. The thin fluid film between faces resists the rotational motion, generating additional heat proportional to fluid viscosity and speed. In low-viscosity services like water, viscous shear is negligible compared to rubbing heat. In high-viscosity oil services, it can become significant — but for most calculation purposes, the rubbing heat formula captures the dominant source.
Why PV Limits Are Only a Screening Tool
Engineers often reach for PV values as a shortcut — if the pressure-velocity product stays below the published limit, the seal should be fine. The problem is that most PV limit data comes from 100-hour tests on a single seal size at 1800 RPM in warm water, then gets extrapolated to two-year service life with no validation. Each manufacturer runs its own test protocol, so you cannot compare one manufacturer’s PV limits with another’s.
PV limits tell you whether you are in the ballpark. The full heat generation formula tells you the actual thermal load. For engineering decisions — sizing a cooler, specifying flush flow, or diagnosing an overheating seal — you need the formula.
The Face-Generated Heat Formula
Face-generated heat comes from one equation:
Q = f x Pf x V x A
Where Q is the heat generated at the seal faces (in watts or Btu/hr), f is the friction coefficient, Pf is the net face pressure, V is the mean sliding velocity, and A is the seal face contact area.
Breaking Down Each Variable
Friction coefficient (f): For carbon vs. silicon carbide or tungsten carbide in clean liquid service, 0.07 is a reliable starting point. Dry or poorly lubricated conditions push f above 0.1. Abrasive slurries can drive it to 0.2 or higher. The friction coefficient is the most judgment-dependent variable in the formula — if you have seal manufacturer test data for your specific conditions, use it.
Net face pressure (Pf): This is not simply the sealed pressure. Face pressure combines hydraulic loading and spring force:
Pf = (P1 – P2) x (b – k) + Psp
Where k is the pressure gradient factor (typically 0.5 for standard assumptions), P1 – P2 is the differential pressure across the seal, b is the balance ratio, and Psp is the spring pressure (usually 20-30 psi for standard single springs).
Mean sliding velocity (V): V = pi x Dm x N / 60, where Dm is the mean face diameter and N is the shaft speed in RPM.
Face contact area (A): A = pi/4 x (Do^2 – Di^2), where Do and Di are the outer and inner diameters of the seal face contact band.
How Balance Ratio Changes the Calculation
The balance ratio (b) is a design lever that directly controls heat generation. An unbalanced seal typically has b = 1.0 or higher, meaning the full hydraulic pressure acts on the faces. A balanced seal reduces b to 0.65-0.85, cutting the hydraulic closing load by 15-35%.
Dropping the balance ratio from 1.0 to 0.75 on a 200 psi application reduces the hydraulic closing load by 25% — but since heat follows net face pressure, (P1 – P2) x (b – k) + Psp, heat drops by about 40% with a 25 psi spring. That is why balanced seals run cooler and last longer in high-pressure service.
Worked Example: Calculating Heat for a 2-Inch Seal at 3600 RPM
Here is how I would calculate face-generated heat for a real installation. This is a standard single seal on a process water pump.
Given parameters:
- Shaft size: 2 inches (50.8 mm)
- Speed: 3600 RPM
- Sealed pressure: 150 psi (1.03 MPa)
- Face materials: carbon graphite vs. silicon carbide
- Face OD: 2.625 in (66.7 mm), Face ID: 2.125 in (54.0 mm)
- Balance ratio: 0.75 (balanced seal)
- Spring pressure: 25 psi
Step 1 — Face contact area:
A = pi/4 x (2.625^2 – 2.125^2) = pi/4 x (6.891 – 4.516) = 1.865 in^2
Step 2 — Net face pressure:
Pf = 150 x (0.75 – 0.5) + 25 = 37.5 + 25 = 62.5 psi
Step 3 — Mean sliding velocity:
Dm = (2.625 + 2.125) / 2 = 2.375 in
V = pi x 2.375 x 3600 / (60 x 12) = 37.3 ft/s
(Dividing by 12 converts inches to feet.)
Step 4 — Heat generated:
First, the friction force at the faces:
F_friction = f x Pf x A = 0.07 x 62.5 x 1.864 = 8.2 lbf
Then, power dissipated:
Q = F_friction x V = 8.2 x 37.3 = 306 ft-lbf/s
Converting to thermal units (1 ft-lbf/s = 1.356 W = 4.63 Btu/hr):
Q = 306 x 1.356 = 415 W (1,420 Btu/hr)
Sanity check with temperature rise: For water service at 15 deg F allowable rise, face heat alone requires:
Flush Rate = Q / (500 x deltaT) = 1,420 / (500 x 15) = 0.19 gpm
That is well below the 1 gpm per inch rule of thumb (2 gpm for this seal). The gap is not a mistake — the rule of thumb covers the combined load of face heat plus heat soak from the pump casing, plus a safety margin. Face-generated heat is only one part of the thermal budget. The next section shows how to calculate the rest.
| Seal Size | Speed (RPM) | Balanced | Approx. Face Heat (Btu/hr) |
|---|---|---|---|
| 1.5 in | 1800 | Yes | 200-600 |
| 2.0 in | 3600 | Yes | 1,200-2,500 |
| 2.0 in | 3600 | No | 2,000-4,500 |
| 3.5 in | 1800 | Yes | 2,000-5,000 |
| 4.0 in | 3600 | Yes | 8,000-16,000 |
These ranges assume carbon vs. SiC faces in clean water service with f = 0.05-0.08. Your actual values depend on fluid properties, lubrication regime, and face condition.
Heat Soak: The Other Heat Source
Face-generated heat is only half the thermal picture. In hot services — anything above roughly 200 deg F — heat also conducts from the pump casing through the metal parts into the seal chamber. This is heat soak, and it requires a separate calculation.
The fundamental heat balance for any seal system is: qsoak + qseal – qcooler = 0. In steady state, the cooling system must remove both the heat generated at the faces (qseal) and the heat conducted from the process (qsoak). Missing either source leads to undersized cooling.
The API 682 method estimates heat soak as:
Hs = 12 x S x deltaT
Where S is the seal size in inches and deltaT is the temperature difference between the pump casing and the seal chamber fluid. For a 3.5-inch seal on a 500 deg F pump with barrier fluid at 150 deg F, this gives 12 x 3.5 x 350 = 14,700 Btu/hr. That heat soak alone exceeds the face-generated heat of most seals in that size range.
Correction factors refine this estimate. A speed factor of (RPM/1800)^0.26 adjusts for shaft speed. A material factor ranges from 1.0 for stainless steel to 2.3 for carbon steel (higher thermal conductivity means more heat soak). Viscosity and fluid type factors further adjust the baseline. These are estimation tools, not precise values — but they get you within engineering accuracy for system sizing.
The face-generated heat term (qseal) is often the most uncertain variable in the system. Calculating it from first principles — rather than assuming a rule-of-thumb value — prevents undersized cooling that leads to premature seal failure.
Connecting Heat Load to Cooling Decisions
The calculated total heat load — face heat plus heat soak — directly determines your piping plan selection and cooling hardware.
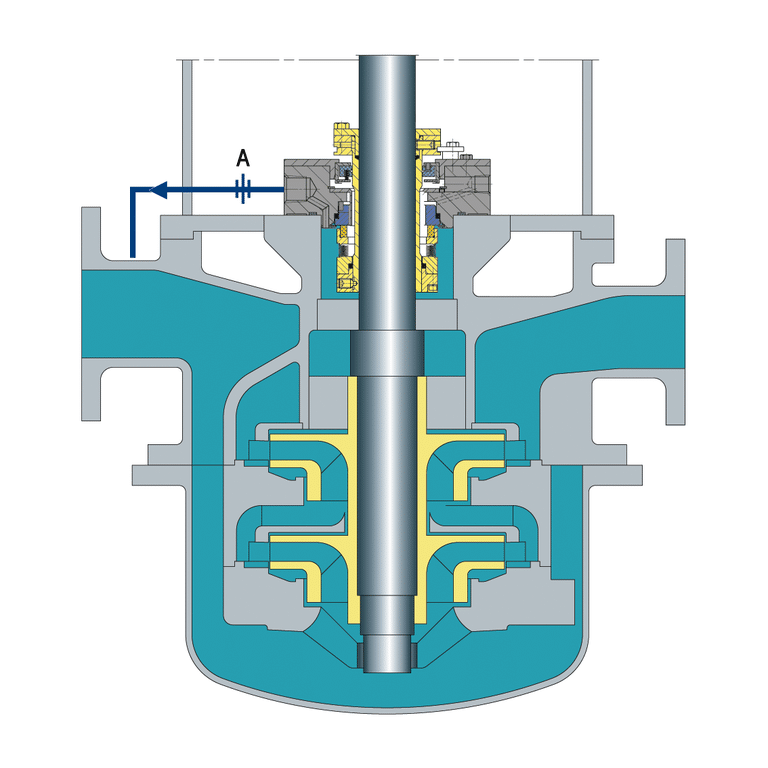
For single seals in moderate services, Plan 11 (recirculation from pump discharge) handles heat loads where the process fluid itself can absorb the thermal energy without exceeding temperature limits that cause heat checking on the seal faces. When the process fluid temperature is too high, Plan 21 adds a cooler in the recirculation loop. Plan 23 uses a closed loop driven by a pumping ring for higher-temperature applications.
For dual seals, the critical threshold is Plan 53B capacity. Most Plan 53B systems remove 8,000 to 12,000 Btu/hr with target barrier fluid supply temperatures around 120 deg F. If your total heat load exceeds that range, you need Plan 54 — an externally pressurized and cooled barrier fluid system with essentially unlimited heat removal capacity.
The flush flow rate calculation uses the total heat load — face heat plus heat soak — as its input. Flush Rate = Q_total / (500 x SG x Cp x deltaT), where SG and Cp are the specific gravity and specific heat of the flush fluid and deltaT is the allowable temperature rise — 5 deg F for high vapor pressure hydrocarbons, 15 deg F for water and low vapor pressure hydrocarbons, 30 deg F for oils. Skipping the heat calculation and defaulting to the “1 gpm per inch” rule works for average conditions but can leave you undersized in hot service where heat soak dominates the thermal budget.
I’ve seen this failure pattern dozens of times: the calculated heat at the faces checks out fine, but the seal still fails in months rather than years. One refinery case involved a hot oil pump running well below best efficiency point. The heat calculation was within limits, but off-BEP operation caused shaft deflection that distorted the seal faces mechanically. Heat calculation is necessary — but it is the starting point, not the complete answer.
What to Do Next
Run the face-generated heat formula for your specific seal installation before accepting any rule-of-thumb flush rate or cooler size. Compare your result against the quick-reference table above as a sanity check. If the pump handles hot service above 200 deg F, add the heat soak calculation to get the total thermal load.
The number you calculate determines whether a simple Plan 11 keeps the seal cool or whether you need the heat removal capacity of a Plan 53B or Plan 54. Getting this right at the design stage prevents the overheating failures that account for a disproportionate share of premature seal replacements. And if the seal still fails after the thermal analysis checks out — look at the pump operating point, not the seal.