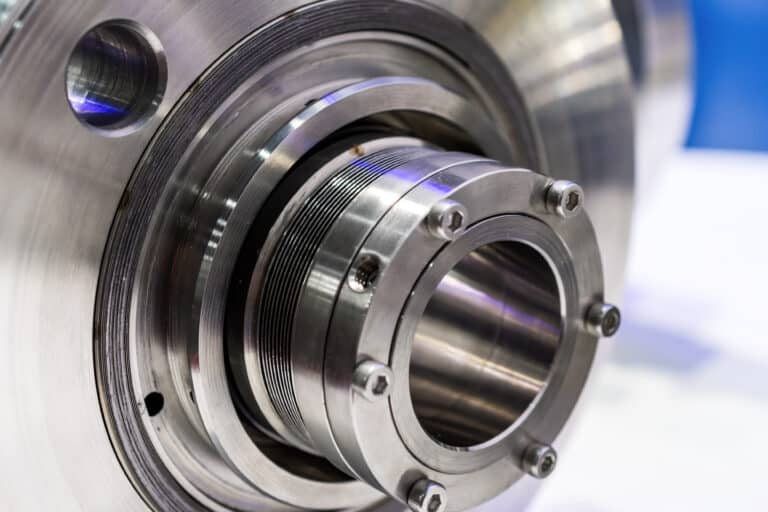
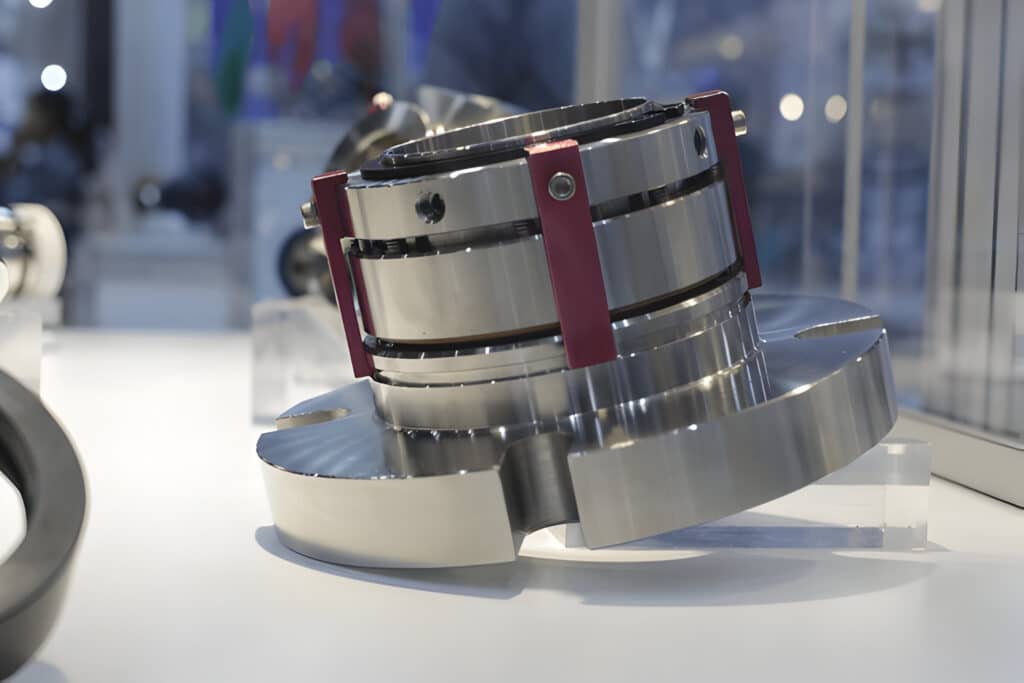
Dry running mechanical seals are sealing devices designed to operate without an external liquid lubricant between the seal faces. They survive the friction and heat that would destroy a conventional wet seal by pairing specialized face materials with a non-liquid lubrication source — gas, the process vapor, or none at all. This page is an awareness-level overview; diagnostic signs, prevention, material selection, and heat calculations are covered on the linked sister pages.
What Are Dry Running Mechanical Seals
A dry running mechanical seal is a rotating shaft seal engineered to function with no liquid film between its primary stationary and rotating faces. A conventional wet seal relies on a thin film of water, oil, or barrier fluid for lubrication and cooling. A dry running seal substitutes a gas film, the process vapor, or self-lubricating face materials.
They appear most often where injecting a liquid into the seal area is impractical: sterile pharmaceutical reactors, vapor-phase service, hot dry-gas duty, and compressors or pumps that cannot tolerate water.

How Do Dry Running Mechanical Seals Work
A mechanical seal — wet or dry — uses two flat faces pressed together by spring force and hydraulic pressure. Leakage is controlled by the flatness of those faces and the film between them. In a wet seal that film is a liquid; in a dry seal it is gas, the process vapor, or a self-deposited solid lubricant from the face material.
The faces are still lapped to within 1–2 helium light bands, and springs and balance ratios still load them. What changes is the lubrication mechanism: the design accepts a thinner, hotter film and uses materials and geometry built to survive it.
Friction heat must escape through the housing, fins, or gas flow. If it cannot, the faces distort, the carbon glazes, and the seal fails. “Dry running” is therefore a design specification, not a mode any mechanical seal can survive.

How Do Dry Running Seals Achieve Lubrication Without Water?
A seal that runs without water still needs lubrication and cooling — those functions shift to a different source. Three methods are used in practice, each fitting a specific equipment class and service condition; process fluid lubrication, a wet-seal arrangement, is listed alongside them for contrast.
| Method | Lubrication Source | Typical Service | Key Limitation |
|---|---|---|---|
| Dry Gas Seal (non-contacting) | Pressurized gas film (process gas or nitrogen) | Dual gas-lubricated pump seals; compressors and gas-handling equipment | Requires clean, dry, regulated gas supply |
| Process Fluid Lubrication | The pumped liquid itself (e.g. API Plan 01) — a wet seal, not dry running | Clean fluids at moderate temperature and pressure | Fails with abrasives, vaporization, or poor-lubricity fluids |
| Self-Lubricating Material Pairings | Solid lubricant film from carbon graphite or DLC | Intermittent dry running, vacuum, vapor-phase service | Brief tolerance only; sustained dry running still wears |
| API Piping Plans 72 / 74 / 75 / 76 | Buffer or barrier gas around a dual seal | Volatile, toxic, or fugitive-emission-controlled service | Requires gas supply infrastructure and monitoring |
Dry Gas Seals (Non-Contacting): Pressurized Gas Film Mechanism
A dry gas seal keeps the rotating and stationary faces fully separated by a thin film of pressurized gas, usually filtered process gas in compressors and nitrogen in pumps. There is no face contact during normal operation, so wear in the conventional sense does not occur.
The gas film is generated by spiral grooves etched into the rotating face. As the shaft spins, the grooves act like miniature pumps, drawing gas inward and compressing it against a sealing dam — enough pressure to lift the stationary face off the rotating one. The resulting gap is about 0.005 mm, roughly one-fourteenth the thickness of a human hair. Small enough for near-zero leakage, large enough to eliminate face contact.
In rotating equipment the gas-film principle is most associated with centrifugal compressors, but the same non-contacting design also appears on dual gas-lubricated mechanical seals in demanding pump services — toxic, volatile, or high-purity duties where introducing any flush liquid, or letting process fluid escape, is unacceptable.
Which of the two a given machine needs is its own decision, worked through in mechanical seal vs dry gas seal.

Process Fluid Lubrication: When Process Fluid Itself Can Lubricate
The pumped fluid can also serve as the seal lubricant, but in liquid form that makes it a wet seal. API Plan 01 is not a dry-running method: the pump’s own internal passages route liquid from the discharge side back to the seal chamber, so the faces run on a liquid film. No external piping or flush water.
API Plan 01 works when three conditions hold: the fluid is clean enough not to abrade the faces, cool enough not to vaporize at the chamber, and lubricious enough to form a hydrodynamic film. Clean cool water, light hydrocarbons, and many process oils qualify; abrasive, vaporizing, or poor-lubricity fluids do not.
Self-Lubricating Material Pairings: Graphite-Based + DLC Coatings
The second method generates the lubricating film from the face material itself. Carbon graphite is the original self-lubricating face: as the seal runs, microscopic graphite particles transfer to the mating face and deposit a thin solid lubricant film. The seal is briefly lubricated by its own wear products.
Carbon graphite is what lets a mechanical seal “run dry” for 10–30 seconds without instant failure — and also why dry-running tolerance has hard limits. Eventually the carbon glazes, the film fails, and the faces grind.
Modern variations extend the principle. Graphite-loaded silicon carbide combines SiC’s hardness with embedded graphite for in-situ lubrication; DLC (diamond-like carbon) coatings give a low-friction, wear-resistant surface that tolerates marginal lubrication. None of these replace external lubrication for continuous service — they are insurance for the moments external lubrication fails.
API Piping Plans for Gas-Lubricated Seals: Plan 72 / 74 / 75 / 76 References
For volatile, toxic, or emission-regulated services, a single dry-running face is not enough. The answer is a dual seal supported by an API piping plan that delivers a gas buffer or barrier between the two seals.
- Plan 72 — Buffer Gas (unpressurized). Buffer gas (usually nitrogen) is supplied between the inner and outer seals at a pressure below chamber pressure. It does not block inner-seal leakage; it dilutes the leakage and carries it to a vent. Used when some leakage is acceptable but it must not reach atmosphere.
- Plan 74 — Barrier Gas (pressurized). Barrier gas is held at least 25 PSI (≈1.7 bar) above chamber pressure, blocking process fluid from reaching the outer seal. Used when zero leakage to atmosphere is required — toxic chemicals, contained pharmaceutical service. Tradeoff: low-rate gas leakage into the process must be acceptable.
- Plans 75 / 76 — Containment. Plan 75 collects condensable leakage from the inner seal of a dual seal with a dry-running containment seal; Plan 76 vents non-condensable leakage to flare. Both manage what escapes past the inner seal.
Features and Advantages
Dry running seals trade flush water and support piping for face-material engineering and heat-dissipation paths:
- Specialized face materials. Carbon graphite, silicon carbide, tungsten carbide, graphite-loaded SiC — chosen for low friction, high thermal conductivity, and self-lubricating behavior under starved-film conditions.
- Engineered heat path. Finned glands, conductive metal paths, and (in some designs) directed gas flow carry away the friction heat a flush would otherwise remove.
- No external flush water. Eliminates the cost, plumbing, and contamination risk of a seal-water system along with its auxiliary failure modes.
- Reach into services a wet seal can’t enter. Vacuum, vapor-phase, and high-temperature applications where a liquid film cannot physically exist — dry running is the only option, not a compromise.
Applications of Dry Running Mechanical Seals
- Mixers and agitators in pharmaceutical reactors, food-grade tanks, and chemical agitators — flush water would contaminate product or the tank top has no flush plumbing.
- Pumps on viscous or abrasive fluids — slurry and high-viscosity service where flush water would dilute the product or be destroyed by abrasives.
- Vacuum and high-temperature service — distillation column bottoms and vapor-phase reactors where a liquid film cannot exist at the faces.
- Flue gas desulfurization (FGD) systems — scrubber-service slurry pumps and agitators where harsh chemistry and no clean-water supply make dry running the practical default.
When Dry-Run Conditions Are Unintended — Cross-References
A seal designed to run dry differs from a wet seal that has unintentionally lost its flush. The pages below cover that second case:
- Suspect a seal is running dry but shouldn’t be — diagnostic checklist (damage patterns, operational symptoms, survival window): signs of a dry-running mechanical seal in a pump.
- Face-material selection where intermittent dry running is expected: materials for dry-running mechanical seals.
- Engineering calc for friction heat in a dry-running configuration: how to calculate heat generation in a dry running seal.
FAQs
Four common questions: survival limits, the wet-vs-dry distinction, the gas-seal subset, and what support hardware is still required.
Can a Standard Wet Mechanical Seal Survive Brief Dry Running?
Briefly. Most wet seals tolerate 10 seconds to 2 minutes of dry running before the carbon face glazes and the elastomers heat-set. Survival depends on face material, speed, and chamber temperature. Designed dry-running seals operate continuously without that limit — by changing materials, geometry, and lubrication strategy, not by being more forgiving versions of the same seal.
What Is the Difference Between Wet and Dry Mechanical Seals?
Wet seals rely on an external liquid film — water, oil, barrier fluid — for lubrication and cooling. Dry seals substitute a gas film, the process vapor, or a self-deposited solid lubricant from the face material. The faces, springs, and basic layout are similar; the lubrication source, materials, and supporting piping change.
Are Dry Gas Seals the Same as Dry Running Seals?
Not exactly. A dry gas seal is one type of dry-running seal — the non-contacting variety, with spiral-groove gas-film lubrication, most familiar on compressors but also built as a dual gas-lubricated seal for pumps. Dry-running seals as a category also include contacting designs that rely on process vapor or self-lubricating materials. All dry gas seals are dry-running; not all dry-running seals are gas seals.
Do Dry Running Seals Need Any Support System?
Dry gas seals need a clean, dry, regulated gas supply and usually a monitoring panel. Dual seals running on API Plan 72/74/75/76 need the corresponding gas supply, vent, or containment piping. “No flush water” is not the same as “no support system.”