Use EPDM in a hydrocarbon pump and the secondary seal swells past its groove within weeks. Use FKM in a hot-water or steam service and it cracks before the next maintenance interval. FKM and EPDM occupy the same mechanical-seal O-ring slot, but their failure modes are largely mirror images: most fluid families that protect one destroy the other. The right material is determined by process fluid first, temperature second.
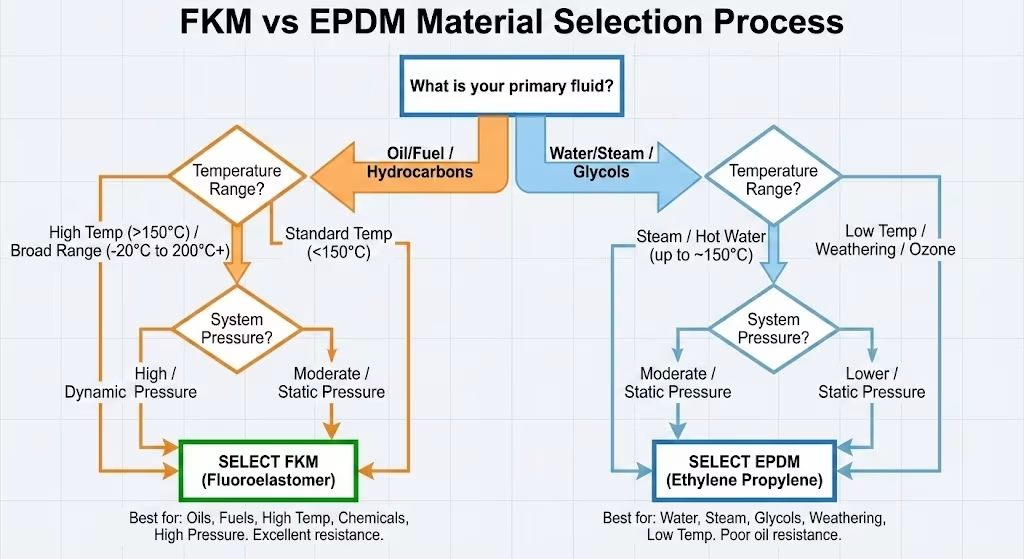
Which Elastomer Material Should You Choose: FKM or EPDM?
Choose FKM when your application involves oils, fuels, or continuous temperatures above 150C. Choose EPDM for water, steam, condensate, or sub-zero environments. This single decision rule covers most mechanical seal applications.
Quick Selection Guide
| Application | Recommended | Why |
|---|---|---|
| Hot water / Steam | EPDM | FKM degrades via hydrolysis |
| Petroleum oils and fuels | FKM | EPDM swells and fails |
| High temperature (>150C) | FKM | EPDM max is 150C |
| Sub-zero cold (-40C) | EPDM or FKM GLT | Standard FKM only to -20C |
| Aggressive chemicals | FKM (GF grade) | 70% fluorine content |
| Food & beverage (water-based) | EPDM | FDA grades available |
| HVAC systems | EPDM | Water resistant; cost-effective |
The Key Difference in One Sentence
FKM is the chemical and oil resistance champion. EPDM is the water, steam, and cold environment specialist.
The fluorine atoms in FKM create strong carbon-fluorine bonds that resist petroleum products and most chemicals. EPDM’s ethylene-propylene backbone provides exceptional stability in water-based environments where FKM would degrade.
What Are the Key Property Differences Between FKM and EPDM?
FKM handles higher temperatures. EPDM offers better flexibility in cold conditions and superior tear resistance. These mechanical differences often determine which material suits your pump application.
Temperature Performance Comparison
| Property | FKM | EPDM |
|---|---|---|
| Standard range | -26C to +205C | -40C to +150C |
| Low-temperature limit | -20C (GLT grade to -40C) | -50C |
| High-temperature limit | 205C continuous, higher for short periods at reduced life | 150C (steam grades to 200C) |
| Best for | Continuous high-heat operation | Cold starts and sub-zero environments |
FKM is serviceable in continuous heat of up to 205C and in short excursions above that at reduced service life. This makes it the clear choice for applications like hot oil systems and high-temperature chemical processes.
EPDM operates reliably at temperatures as low as -50C. For cold climate installations or cryogenic adjacent equipment, EPDM maintains flexibility where standard FKM would become brittle.
Mechanical Properties
| Property | FKM | EPDM |
|---|---|---|
| Hardness (Shore A) | 75-90 | 70-90 |
| Max Pressure | Set by hardness, gap and back-up rings | Set by hardness, gap and back-up rings |
| Compression Set | Excellent | Good |
| Tear Resistance | Good | Excellent |
| Abrasion Resistance | Good | Excellent |
Pressure capability depends on hardness, extrusion gap and back-up rings as well as elastomer type. Both materials are offered at 90 Shore A for high-pressure pump applications.
EPDM’s superior tear resistance and elongation at break (300% to 600%) make it more forgiving during installation. This matters for maintenance teams handling frequent seal changes.
Chemical Resistance Overview
| Chemical Category | FKM Rating | EPDM Rating |
|---|---|---|
| Petroleum oils | Excellent | Poor – swells |
| Fuels/Gasoline | Excellent | Poor – fails |
| Hot water/Steam | Poor – degrades | Excellent |
| Ketones/Acetone | Poor | Excellent |
| Acids (dilute) | Excellent | Good |
| Ozone/UV | Excellent | Excellent |
| Alcohols | Poor (methanol) to Excellent | Excellent |
The compatibility table reveals a critical pattern: where FKM excels, EPDM usually fails, and vice versa. This is why specifying the wrong elastomer causes rapid seal failure rather than gradual wear.
Why Does FKM Fail in Water and Steam Applications?
FKM fails in hot water and steam because of hydrolysis – a chemical attack that breaks down the polymer structure. This is not a quality issue or manufacturing defect. It is fundamental chemistry.
The Hydrolysis Mechanism
As one engineer on Eng-Tips explained: “The hot water has a relatively high concentration of OH- radicals, which tend to attack crosslinks both between and along the polymer chain.”
This mechanism means standard FKM seals in steam service will degrade regardless of brand or quality. The OH- radicals cause chain scission, breaking the polymer into shorter segments. The seal loses elasticity, develops cracks, and eventually fails.
For water, steam, and condensate applications, EPDM is not just acceptable – it is the only correct choice. Using FKM in these conditions leads to premature failure that no amount of seal quality can prevent.
When EPDM Is the Only Correct Choice
EPDM should be specified for:
- Hot water service above 60C
- Steam environments up to 150C (special grades to 200C)
- HVAC and water treatment systems
- Boiler feed applications
- Condensate return lines
O-rings with EPDM as the base polymer reliably retain their properties in hot water and steam up to about 150C, and special steam grades up to 200C. No other common elastomer matches this performance in water-based environments.
The Peroxide-Cured FKM Exception
Peroxide-cured FKM offers improved resistance to steam compared to standard bisphenol-cured FKM. Engineers recommend this variant when an application requires both chemical resistance and occasional steam exposure.
However, peroxide-cured FKM still does not match EPDM’s water resistance. Consider it only when you need FKM’s chemical resistance and can tolerate occasional (not continuous) steam contact.
What About Cost: Is FKM Worth the Premium?
FKM is often the most expensive of the common rubber types. This premium reflects its chemical makeup and manufacturing complexity. But higher cost does not mean universal superiority.
Price Positioning
FKM rubber is a premium product that typically costs significantly more than EPDM. This price difference makes material selection important for budget-conscious projects.
EPDM offers excellent value when the application suits its properties. Paying the FKM premium for a water treatment application wastes money and could actually reduce seal life.
When to Invest in FKM
FKM justifies its premium cost in these scenarios:
- High-temperature continuous operation above 150C
- Oil and fuel exposure in pumps and fuel systems
- Aggressive chemical environments requiring 70% fluorine grades
- High-pressure applications that also involve oils, fuels or chemicals
- Applications where seal failure creates safety or environmental risks
For these conditions, FKM’s performance advantages outweigh the higher material cost. Seal replacement costs and downtime quickly exceed the material price difference.
When EPDM Delivers Better Value
EPDM provides superior value for:
- Water-based applications including potable water systems
- Steam service and boiler applications
- Cold temperature operation below -30C
- Budget-conscious projects with suitable operating conditions
- High-volume applications where material cost matters
Choosing EPDM where appropriate saves money without sacrificing performance. In fact, using EPDM for water applications actually improves seal life compared to FKM.
Application Decision Matrix: FKM vs EPDM by Industry
Each industry has typical operating conditions that favor one elastomer over the other. Use these recommendations as starting points, then verify against your specific fluid and temperature requirements.
Water Treatment and HVAC
For water treatment and HVAC service, EPDM is the standard choice. Water treatment facilities and HVAC systems primarily handle water at various temperatures. EPDM’s water resistance and cost-effectiveness make it the standard choice for these industries.
For mechanical seals for centrifugal pumps in water service, EPDM O-rings provide reliable sealing without the hydrolysis concerns of FKM.
Chemical Processing
FKM (with grade specified by the chemicals involved) is the standard for chemical processing service. Chemical processing environments typically involve aggressive fluids that require FKM’s chemical resistance. Match the FKM grade to your specific chemical exposure – GF grades for the most aggressive applications.
Exception: Water-based chemical processes may use EPDM if no oil or solvent contamination is possible.
Food and Beverage
Water-based products and cleaning processes favor EPDM. FDA-compliant EPDM grades are available for food contact applications.
Oil and fat exposure in food processing requires FKM. Vegetable oils, animal fats, and oil-based flavorings will swell EPDM seals.
Pharmaceutical
Water and steam sterilization processes favor EPDM. Steam-in-place (SIP) cleaning cycles use steam that would degrade FKM seals.
Hydrocarbon and chlorinated solvents require FKM. Ketones, esters and methanol attack FKM; specify FFKM, or EPDM for ketones and methanol.
Conclusion
Selecting between FKM and EPDM becomes straightforward once you know your operating conditions. Identify your fluid type, temperature range, and pressure requirements, then match them to the material properties in this guide.
Need help specifying the right elastomer for your mechanical seal? Our engineering team can review your application requirements and recommend the optimal material for your operating conditions.