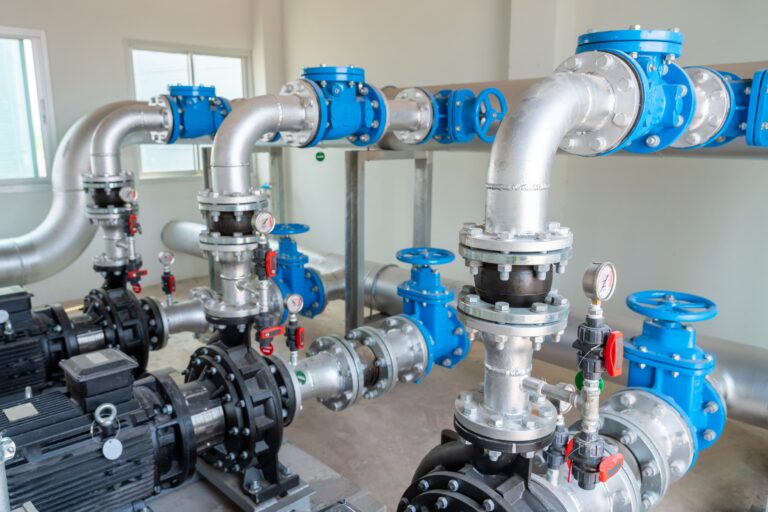
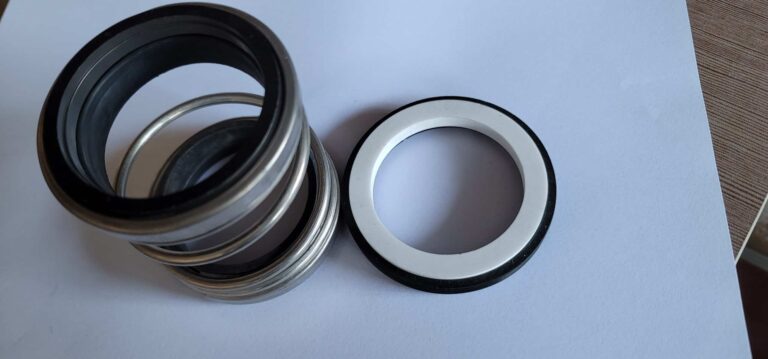
You just spent four hours pulling a vertical multistage pump apart and installing a new seal, and it’s dripping before the motor reaches full speed. Before you blame the seal, consider this: 30-40% of premature seal failures trace back to operating conditions the seal never caused, and another 20-30% come from installation errors that have nothing to do with seal quality. In a vertical multistage pump, the situation gets worse. Gravity, thrust balance, multi-stage casing alignment, and air pockets in the seal chamber create failure modes that horizontal pumps simply don’t have.
The most common mistake I see is applying generic seal troubleshooting to vertical multistage pumps. Air entrapment gets all the attention, but it’s one of at least five vertical-specific root causes for post-replacement leaks. When the leak appears tells you where to look.
Diagnosing by Leak Timing: What Your Symptom Pattern Tells You
A leak that starts on the first revolution points to a completely different problem than one that develops after three weeks of operation. I use a three-category system based on when the leak appears, because each timing window maps to a distinct set of root causes specific to vertical multistage pumps.
| Leak Timing | Root Cause Category | Where to Look First |
|---|---|---|
| Immediate (startup) | Installation error | Setting height, O-rings, face damage, torque |
| Days to weeks | Pump condition | Wear rings, thrust balance, shaft deflection |
| Intermittent (comes and goes) | Operational / venting | Air entrapment, off-BEP operation, drain port |
Immediate leaks are the easiest to diagnose because the evidence is fresh. Short-term leaks are the most frustrating because the seal appeared to work at first — the pump’s mechanical condition is degrading the new seal from the moment you start it. Intermittent leaks are the trickiest because the symptom disappears when you go to investigate.
Start with the timing, narrow to the category, then work through the specific checks below.
Immediate Leaks: Installation Errors to Recheck
If the seal leaks within minutes of startup, something went wrong during installation. Don’t assume you need to start over — work through these checks in order before pulling the pump again.
Setting height and compression. Vertical multistage pumps stack multiple stages, and the cumulative tolerance stack-up can shift the seal’s axial position. On Grundfos CR/CRN units, the cartridge seal must be pressed onto the shaft and tightened to 35 Nm with the ring insert. Miss that torque value, and the seal faces either under-compress (immediate leak) or over-compress (premature heat failure within hours). If you’re working on a non-cartridge seal, verify the setting height against the manufacturer’s drawing — not the old seal you removed, which may have been wrong too.
O-ring and secondary seal damage. Every static O-ring and gasket must be replaced during overhaul, not inspected and reused. I’ve pulled apart leaking installations where the technician reused an O-ring that “looked fine” — under magnification, the compression set was clearly visible. Also check for nicks on dynamic O-rings. If the shaft end wasn’t cleaned and smoothed before pressing the seal on, the O-ring likely dragged across a burr.
Seal face contamination. Fingerprints, shop dust, or a single fiber from a shop rag on the lapped faces will break the fluid film. Seal faces are lapped flat to within 0.00003 inches — the rotating and stationary faces run with a gap 75 times narrower than a human hair during operation. Any contamination particle wider than that gap holds the faces apart and creates a direct leak path.
Wrong seal type or dimensions. If you switched brands or went from OEM to aftermarket, verify that the seal dimensions match the vertical multistage pump’s requirements exactly. A seal that’s dimensionally close but not identical can seat in the chamber without obvious interference and still leak because the balance ratio or face width is slightly off.
Leaks Within Days or Weeks: Pump Condition Problems
The seal installation was correct, startup looked clean, and the leak showed up on the third shift or the following week. The new seal is being destroyed by a pump condition that existed before you opened it up — and this category catches experienced technicians off guard.
Worn Wear Rings and Seal Chamber Pressure
Wear rings create a close-clearance barrier between the impeller and casing to prevent discharge-to-suction recirculation. In vertical multistage pumps, the rear wear rings also work with balance holes to manage axial thrust by controlling pressure behind the impeller. When wear ring clearances open up beyond spec, two things happen simultaneously: volumetric efficiency drops, and the pressure-balancing mechanism fails.
That failed pressure balance shifts axial thrust onto the shaft — and onto your new seal. The seal faces experience loading they weren’t designed for, and the face contact pattern changes from uniform to edge-loaded. Within days, you get accelerated wear on one side of the carbon face.
Manufacturers recommend replacing wear rings when clearances have increased by 40% of the original specification. API 610 provides baseline clearances: for rings up to five inches in diameter, minimum clearance is 0.010 inches plus 0.002 inches per inch of diameter. If nobody checked wear rings during the seal replacement, the pump may look fine but be silently destroying every new seal you install.
Thrust Imbalance and Shaft Movement
Shaft deflection in vertical pumps is the bending that occurs when liquid velocity around the impeller isn’t uniform. In multistage vertical pumps, shafts can extend many feet through multiple stages, amplifying deflection effects. A seal that passes a bench test will fail in the pump because in-situ shaft movement exceeds the seal’s radial tolerance.
API 610 sets maximum shaft deflection at the seal face at 0.002 inches. Before you start, make sure the shaft runout is within that limit — check it with the pump assembled but not pressurized. If deflection exceeds spec, no seal will survive regardless of quality.
One detail technicians rarely consider: if you replaced a rotating seal with a stationary type (or vice versa), you changed the pump’s thrust profile. Stationary seals generate larger thrust loads than rotating seals at identical chamber pressures because the balance diameter is larger — typically 0.625 to 1.0 inches above shaft OD versus 0.5 to 0.625 inches for rotating designs. That seemingly small difference compounds across multiple stages at high pressures. On a pump that was already marginal on thrust balance, switching seal types can push it over the edge.
Intermittent Leaks: Operational and Venting Issues
An intermittent leak — one that appears under certain conditions and disappears under others — points to operational factors rather than hardware failure. These are the hardest to catch because the seal looks fine when you inspect it.
Air Entrapment in the Seal Chamber
In a vertical multistage pump, the seal chamber sits at the top of the assembly. It’s the high point. Any air in the system migrates there and collects around the seal faces. The Amherst, NY wastewater plant fought this exact problem: flush water was flowing through the seal chamber, but entrained air accumulated in a pocket around the seal faces. The flush water passed through the air pocket without displacing it. The seal faces ran dry inside the air bubble even though flush flow looked normal on the gauge.
The fix was simple — float-needle valves installed above the seal chambers to continuously vent trapped air. But the diagnostic lesson is critical: if your seal leaks during startup or after the pump has been idle, and the leak slows or stops after extended running, air entrapment is the most likely cause. Verify that the seal chamber vent path is clear and functional before you do anything else.
Operating Off-BEP and Drain Port Problems
Centrifugal pumps don’t operate smoothly below about 50% of Best Efficiency Point (BEP) flow. Below that threshold, vibration and radial loading spike — both are seal killers. If the leak correlates with low-flow or deadhead conditions, the pump’s operating point is the problem, not the seal.
A less obvious intermittent cause: missing or blocked drain ports. In vertical installations, gravity drives fluid accumulation in the shaft column above the seal. Without a functional drain path, that fluid column builds pressure on the seal’s atmospheric side. The seal overpressurizes from the wrong direction — it looks like a seal failure, but it’s a system design problem. Check whether the drain port exists, whether it’s open, and whether the piping routes to an appropriate drain. If you skip this step, you’ll be back in a week with the same leak.
Before You Pull the Pump: External Diagnostic Checks
Pulling a vertical multistage pump is expensive — hours of labor, crane time, potential piping modifications. Before committing to a full teardown, run through these external checks to narrow the root cause.
Seal chamber pressure. Install a gauge on the seal flush line or chamber port. Compare the reading to the expected value from the pump curve. Low pressure suggests worn wear rings or balance issues. Abnormally high pressure may indicate a blocked vent or drain.
Vibration baseline. Take vibration readings at the seal gland and at each bearing housing. Elevated vibration at the seal location points to shaft deflection or misalignment. Elevated vibration at the bearings suggests a thrust or balance problem propagating through the machine.
Visual leak pattern. Steady drip from the seal gland = face leak. Weeping from the gland bolts or between the gland and the housing = O-ring or gasket leak. Spray pattern = catastrophic face separation. Each pattern tells you whether you need to replace the seal or just address the secondary seals.
Flush system verification. Confirm flow rate, pressure, and temperature on the flush line. A partially blocked flush orifice or a closed valve that someone forgot to reopen after maintenance will starve the seal of cooling and lubrication. This is a five-minute check that prevents a four-hour teardown.
Shaft axial play. With the pump de-energized, feel for axial movement at the coupling end. Measurable play indicates thrust bearing wear — and every millimeter of axial float translates to changing compression on the seal faces.
Prevention Starts Before the Seal Goes In
The pattern across every root cause above is the same: the seal didn’t fail because it was defective. The seal failed because something about the pump’s mechanical condition or the installation process set it up to fail. A functioning mechanical seal leaks about half a teaspoon per day at normal operating conditions. Anything beyond a slow weep on a vertical multistage pump means something specific is wrong.
Before your next seal replacement, add three checks to your pre-work scope: measure wear ring clearances and replace any ring beyond 40% of original spec, verify shaft runout at the seal face location against the 0.002-inch API limit, and confirm the seal chamber vent and drain paths are clear. These three items catch the root causes that account for the majority of post-replacement leaks in vertical multistage pumps — and they take less time than replacing the seal a second time.