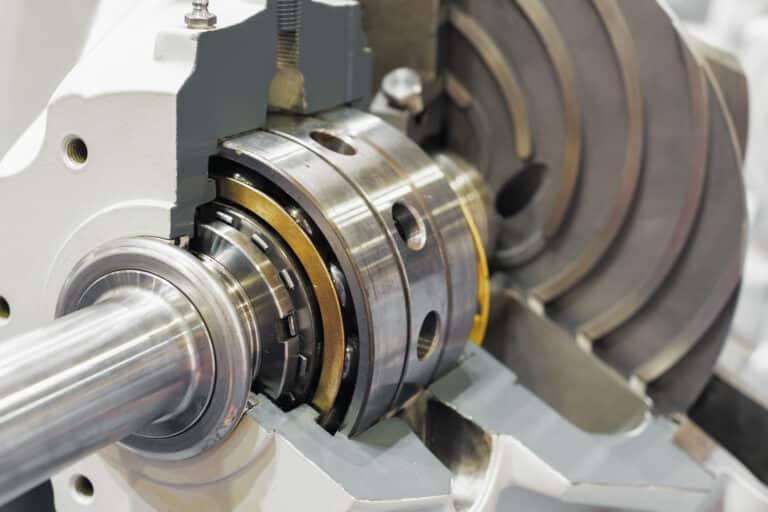
A standard mechanical seal running at 3,600 RPM on a 50 mm shaft sees about 9.4 m/s of peripheral velocity. Double the shaft diameter to 100 mm at the same speed, and that jumps to 18.8 m/s. Push to a multistage boiler feed pump at 6,000 RPM with a 120 mm shaft, and you’re at 37.7 m/s — well into territory where a standard seal specification will fail. The engineering challenge isn’t the RPM on the nameplate. It’s the velocity at the seal face, and everything that velocity does to heat, film stability, and face tracking.
Most available guidance treats high-speed sealing as a binary switch — standard below 25 m/s, special above it. That oversimplification has cost engineers I’ve worked with months of troubleshooting. Speed creates a spectrum of design responses, and the seal that handles 35 m/s competently will self-destruct at 80 m/s.
What Defines a High-Speed Mechanical Seal
Peripheral velocity above 25 m/s is the widely accepted threshold where standard seal designs reach their operating limits. At this speed, frictional heat generation exceeds what conventional cooling can manage, face wear accelerates nonlinearly, and dynamic tracking demands tighter tolerances.
RPM alone tells you nothing useful. A 25 mm shaft at 20,000 RPM produces 26.2 m/s — barely into the high-speed zone. A 200 mm shaft at 5,000 RPM produces 52.4 m/s — a far more severe application. The formula: peripheral velocity (m/s) = pi x shaft diameter (m) x RPM / 60. Always calculate this before specifying a seal.
The transition isn’t a cliff edge. Unbalanced seals are rated up to about 25 m/s and balanced designs are the general rule above about 13.8 bar (200 psi), but the region approaching those limits is where most specification errors happen — unbalanced seals sometimes survive, sometimes don’t, and engineers assume the last success guarantees the next one. Above 25 m/s, mechanical seals can operate up to approximately 150 m/s, but each speed tier demands different design responses.
Design Features That Change at High Speed
At 40 m/s, a seal face generates roughly twice the frictional heat it produces at 20 m/s. Every design modification in a high-speed seal addresses this thermal reality and the dynamic instability that accompanies it.
Face Geometry and Balance Ratio
High-speed seals narrow the sealing face width to approximately 3 mm — roughly half what a standard seal uses. This reduces friction heat but also cuts the margin for face distortion. Face flatness tolerances tighten to 1-2 helium light bands (0.3-0.6 micrometers), and the balance ratio increases to 0.75-0.85. The API 682 standard specifies these parameters for a reason: at high peripheral velocity, even minor face distortion opens a leak path that widens with each revolution.
Spring Configuration and Dynamic Tracking
Stationary spring designs replace rotating spring arrangements above 25 m/s. When springs rotate at high speed, centrifugal force alters their effective load, creating cyclic face loading. Multiple small springs distributed around the seal face provide more uniform loading than a single large spring.
Vibration becomes the dominant failure mechanism at high speed, not face wear. The rotating face wobbles relative to the stationary face, and each revolution delivers an impact load. At 6,000 RPM, that’s 100 impacts per second. Machined impellers produce much less imbalance than cast versions, and operating pumps within BEP becomes non-negotiable. Running even 15% beyond BEP at high speed can halve seal life.
Face Materials for High-Speed Service
Carbon paired with silicon carbide delivers the highest PV limit of any standard material combination at 1,471 bar*m/s in non-lubricating fluids — multiply by 1.5 for lubricating service. That’s nearly six times higher than tungsten carbide against tungsten carbide at 249 bar*m/s. This inverts a common intuition: harder does not mean better at high speed.
Carbon-graphite acts as a self-lubricating bearing surface, with friction coefficients well below hard-hard pairings. SiC provides the wear resistance and thermal conductivity (120-170 W/m*K depending on grade) to conduct heat away from the interface. SiC/SiC hard-hard pairings reach 858 bar*m/s — excellent for abrasive media where carbon would erode, but the friction penalty limits their speed ceiling in clean fluids.
SiC grade matters as much as SiC selection itself. Reaction-bonded SiC offers superior thermal shock resistance for frequent temperature cycling. Sintered SiC with graphite inclusions improves dry-running survivability — critical where momentary loss of lubrication during transients is common. For boiler feed pumps, porous sintered SiC grades with engineered porosity trap lubricating film and support emergency running when flash occurs at the faces.
Temperature limits create hard boundaries. Resin-impregnated carbon maxes out at 275 C, antimony-impregnated carbon extends to 350 C, SiC continues to 1,650 C. For high-temperature, high-speed applications like boiler feed water service, antimony-impregnated carbon against sintered SiC with graphite is the combination I default to.
Contacting vs. Non-Contacting Seals
Liquid-lubricated contacting seals and dry gas seals solve the speed problem through opposite mechanisms. Choosing between them depends on the application, not a universal speed threshold.
Contacting seals operate in a mixed lubrication regime where face loading is only partially supported by the sealed liquid. Frictional heat scales with speed. Their advantage: they work with any process fluid, require no external gas supply, and handle the 25-80 m/s range where most real-world high-speed pump challenges exist.
Gas seals separate faces entirely through hydrodynamic lift-off. Spiral grooves or Rayleigh pad patterns compress gas as faces rotate, maintaining a 2-4 micrometer gap — complete non-contact operation. Heat generation drops to near zero.
The design inversion most guidance misses: gas seals require a minimum circumferential speed of roughly 1.3 m/s to generate sufficient lift-off pressure. Contacting seals degrade with increasing speed; gas seals need speed to function. Gas seals also require clean, dry barrier gas and struggle with slurries above 5% solids. For most high-speed pump applications handling liquid, contacting seals with proper material selection and flush plans remain the correct choice.
Matching Seal Design to Speed Regime
Speed creates three distinct design tiers, each requiring different engineering responses. I’ve used this classification for years, and it eliminates the guesswork that comes from treating high-speed as a single category.
25-50 m/s — Enhanced contacting seals. Most multistage pumps and moderate-speed compressors. Balanced design mandatory. Carbon vs. SiC face pairing handles the PV load. API Plan 23 closed-loop cooling or Plan 21 with a cooler manages the thermal load. Narrow faces (3 mm), stationary springs, perpendicularity tolerances of 5 micrometers or less. A properly specified seal here routinely achieves 36-48 months between repairs.
50-80 m/s — High-performance contacting or gas-lubricated face seals. The transition zone. Contacting seals still work, but thermal management becomes limiting. Barrier fluid systems (API Plan 54) with external cooling may be necessary, and the external barrier skid adds real cost and complexity. Gas-lubricated face seals eliminate frictional heat entirely but require clean gas infrastructure.
80+ m/s — Non-contacting dry gas seals. Above roughly 80 m/s you have left centrifugal-pump service for turbomachinery — integrally geared and between-bearing compressors and high-speed turbines — where non-contacting dry gas seals take over. That regime is a separate equipment class with its own sealing discipline, outside pump mechanical seal selection; for pumps, the 25-80 m/s contacting and gas-lubricated face designs above are the operative tiers.
One power plant I worked with doubled their boiler feed pump MTBR from 20 to 40 months after upgrading from a generic specification to a properly tiered selection matched to actual peripheral velocity and process conditions. The seal model changed, but the real improvement came from getting the speed-regime classification right.
The Speed Spectrum, Not a Threshold
The most expensive seal failures I’ve investigated weren’t caused by wrong seal designs — they were caused by treating speed as a checkbox instead of a design variable. A seal that runs perfectly at 35 m/s will not survive at 65 m/s, even if both fall into the same “high-speed” category on a datasheet.
Start every high-speed specification by calculating peripheral velocity, not reading RPM. Match that velocity to the correct design tier, select face materials with adequate PV margin, and verify that the thermal management plan matches the actual heat load. Get this sequence right, and the seal becomes one of the most reliable components in the system.