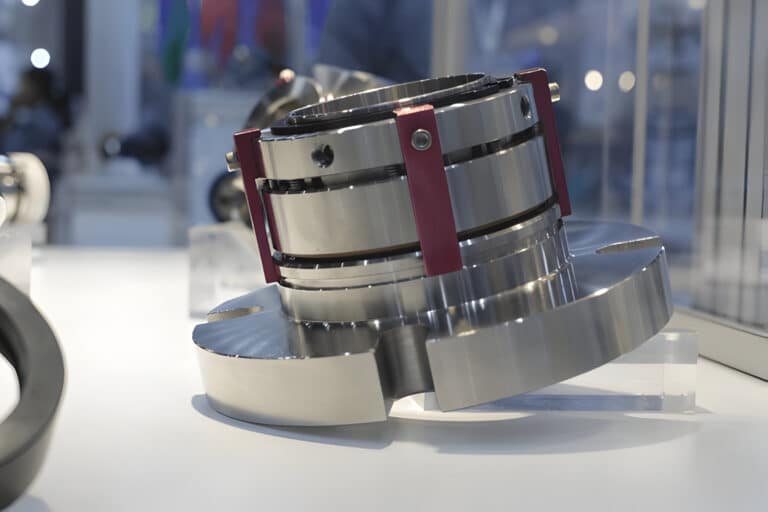
A nuclear power plant main pump in my files ran EPDM secondary seals in a 60 °C, 1.3 MPa water service the material handles easily. The seal still died.
During routine maintenance, the O-ring was wiped down with kerosene and rust remover. Within service hours, the EPDM had swollen, lost groove compression, and started leaking. The maintenance fluids killed it — not the process medium.
That failure is why PTFE vs EPDM for pump secondary seals is not the same question as PTFE vs EPDM for a flange gasket. The top Google results are written for gaskets and valve seats — none answer the pump question: which failure mode can your mechanical seal afford? This guide stays in pump mechanical seal territory — O-rings, wedges, dynamic duty, API 682 — and names the downsides each material hides.
Is PTFE the Same as EPDM? (Thermoplastic vs Thermoset)
PTFE and EPDM are not the same class of material, and treating them as interchangeable rubber-like seals is the first specification error. PTFE — widely known by its DuPont trade name Teflon — is a thermoplastic fluoropolymer. EPDM is a thermoset elastomer.
Why the Classification Controls Every Decision
A thermoset elastomer like EPDM is vulcanized once, forms a cross-linked polymer network, and recovers from deformation — squeeze it into a groove and it pushes back. A thermoplastic like PTFE has a linear chain structure with no memory.
Compress PTFE under sustained load and it reshapes permanently. That is what the industry calls cold flow or creep, and it is not a defect — it is the material class behaving as designed.
Older references sometimes classify PTFE as a “thermoset plastic.” A reader who believes PTFE will spring back like rubber will specify it into dynamic duty and blame the material when the seal fails.
PTFE vs EPDM: Side-by-Side Properties for Pump Secondary Seals
PTFE and EPDM diverge most sharply on property — PTFE wins on temperature and chemistry, EPDM on dynamic recovery and conformability.
| Property | EPDM | PTFE (Teflon) |
|---|---|---|
| Temperature range | -40 °C to 150 °C (peroxide-cured up to ~160 °C) | -200 °C to 260 °C |
| Chemistry (pump fluids) | Water, steam, CIP chemistry, mild acids/alkalis, brake fluids, ketones | Near-universal, pH 0-14 |
| Hydrocarbon exposure | Not recommended — swells, doubles in cross-section | Fully compatible |
| Memory / recovery | Yes — thermoset, springs back | No — cold flow under sustained load |
| Conformability to surface finish | Soft, conforms to imperfections | Stiffer, requires a smooth mating surface |
| Typical pump secondary seal form | O-ring (dynamic and static) | Wedge, V-ring, spring-energized, or static O-ring |
Read this table as a filter, not a verdict. EPDM’s 150 °C ceiling rules it out of hot hydrocarbon service before chemistry enters the discussion. PTFE’s pH 0-14 range is useless on a reciprocating shaft without proper energization and shaft preparation.
Disadvantages of EPDM in Pump Mechanical Seals
EPDM’s fatal weakness in pump service is hydrocarbons. An EPDM O-ring exposed to petroleum oil, diesel, kerosene, or any light hydrocarbon absorbs the fluid and expands — sometimes doubling in cross-section. The O-ring goes gummy, loses groove compression, and the seal collapses.
The Nuclear Pump Case: Maintenance Killed the Seal
The nuclear pump case is the textbook example: the process medium was EPDM-compatible the entire time. What killed the seal was kerosene-based cleaners and petrolatum used during a routine bearing room service.
I’ve seen this failure pattern dozens of times in plants that pick EPDM for cost reasons and then contaminate the groove during a seal swap. When hydrocarbon exposure is even intermittent, a fluoroelastomer like FPM is the correct upgrade — thermoset recovery without EPDM’s hydrocarbon blind spot.
Three Other Limits Before You Specify EPDM
- Temperature ceiling around 150 °C (roughly 160 °C for peroxide-cured grades). Hot boiler feedwater and steam condensate pumps sit right at the edge.
- No resistance to strong oxidizers, chlorinated solvents, or aromatic fuels. Ozone in outdoor installations is also a long-term enemy.
- Not a first-choice material for abrasive services — the softness that lets EPDM conform to a rough surface also makes it vulnerable to nibbling wear on a scored shaft.
Before specifying EPDM for any pump that sees hydrocarbons — even only during maintenance — assume the secondary seal will need to survive that exposure, not just the normal duty.
Disadvantages of PTFE (Teflon) in Pump Mechanical Seals
PTFE’s weaknesses are different in kind from EPDM’s, and they all trace back to its thermoplastic nature. The big three: cold flow, shaft fretting, and the hidden prerequisite that no spec sheet highlights.
Cold Flow Under Sustained Compression
PTFE has no memory. Compressed by bolt torque, thermal expansion, or a spring pack, it stays compressed.
Practitioners describe the symptom this way: the seal works fine on first installation, but break the joint and reinstall the same part and it leaks. The PTFE reshaped to the original clearance and can’t recover to seal the new one.
Wedge-Induced Shaft Fretting
A PTFE wedge sliding on an unhardened pump shaft or sleeve will abrade the surface under dynamic loading — the pump-specific failure mode gasket guides never mention.
AS&P puts it bluntly: PTFE wedges fret sleeves and shafts that aren’t hard-surfaced — plasma coating is the industry prerequisite. I’ve pulled seals where the wedge looked fine but the sleeve had a visible wear groove. The spec sheet said PTFE was chemically right; the shaft wasn’t ready for it.
Higher Cost, Longer Lead Time
PTFE cannot be injection-molded. Parts are machined from billet or compression-sintered, which pushes unit cost higher and extends delivery on custom cross-sections.
What the spec sheet doesn’t tell you is that a PTFE wedge is a system specification, not just a material specification. You are committing to plasma-coated sleeve preparation, a spring-energized design, and tighter groove tolerances. Skip any of those and the chemistry advantage you bought PTFE for becomes irrelevant.
The 5-Parameter Decision Framework
Alan Evans, a 30-year veteran of the sealing industry at A.W. Chesterton, specifies five parameters for secondary seal selection. Applied to pump mechanical seals, they collapse the EPDM vs PTFE question into a decision rule.
- Temperature. EPDM above ~150 °C — move to FKM or PTFE. Below -40 °C — PTFE is the only survivor.
- Chemistry. Hydrocarbons, fuels, chlorinated solvents — EPDM is out. Strong acids, caustics, oxidizers at elevated temperature — PTFE or FFKM.
- Pressure. Standard seal chamber pressures suit both; extrusion resistance matters more once pressure crosses ~100 bar — favor PTFE or add a backup ring.
- Static or dynamic duty. The decisive parameter most spec sheets skip. A static O-ring groove lets you exploit PTFE’s chemistry without paying the cold-flow penalty. A dynamic seal face needs EPDM’s elastomeric recovery — or a spring-energized PTFE design with matching shaft prep.
- Hardness and surface conformity. If the shaft is merely finish-ground, EPDM’s conformability is an advantage. If the hardware is hardened and you need chemical immunity, PTFE becomes viable.
The API 682 standard encodes this logic: Type A and Type B pump seals use elastomeric secondary seals (EPDM, FKM, FFKM), while Type C high-temperature bellows seals use flexible graphite — not PTFE, not elastomer.
The rule: static duty → exploit PTFE’s chemistry. Dynamic duty → exploit EPDM’s recovery. If neither fits, the answer isn’t one of these two materials.
When Neither PTFE nor EPDM Is Right
The five-parameter filter leaves some services in a gap where neither material fits. Hot hydrocarbon pumps in refineries and heat-transfer loops sit above EPDM’s chemistry window and ask a dynamic-duty question PTFE can’t answer without full spring energization and shaft hardening.
Hot Hydrocarbons: Move Up to FKM
FKM gives you EPDM-style thermoset recovery with hydrocarbon and temperature immunity up to around 200 °C — the middle-ground answer when the service crosses EPDM’s chemistry ceiling but doesn’t need PTFE’s full chemical range.
Aggressive Chemistry at Temperature: Move Up to FFKM
For strong acids, amines, high-temperature caustic, or CIP at elevated temperature, FFKM holds thermoset behavior to roughly 275 °C with near-PTFE chemical immunity — the answer when EPDM’s chemistry fails but PTFE’s dynamic behavior is wrong.
When a PTFE Wedge Is the Correct Answer
For dry-running or severely corrosive services, a metal bellows seal or a cartridge seal with engineered shaft preparation is the architecture that makes PTFE work. Specifying the elastomer without specifying the seal architecture is where most premature failures start.
The Bottom Line
Stop asking which material is better. Ask which failure mode your pump can afford.
Static duty, aggressive chemistry — PTFE earns its price if the hardware is prepared. Dynamic duty, mild chemistry — EPDM is the obvious pick if no hydrocarbon touches the groove, maintenance fluids included.
When both materials fail the test, don’t compromise sideways. Move up to FKM for hot hydrocarbons, FFKM for aggressive chemistry at temperature, or flexible graphite inside a metal bellows for the extreme end. The right secondary seal is the one whose failure mode the service will never trigger.