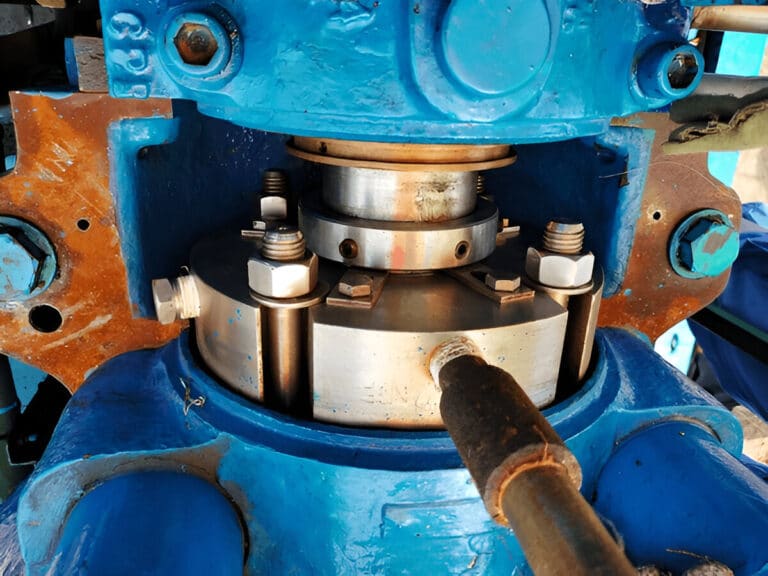
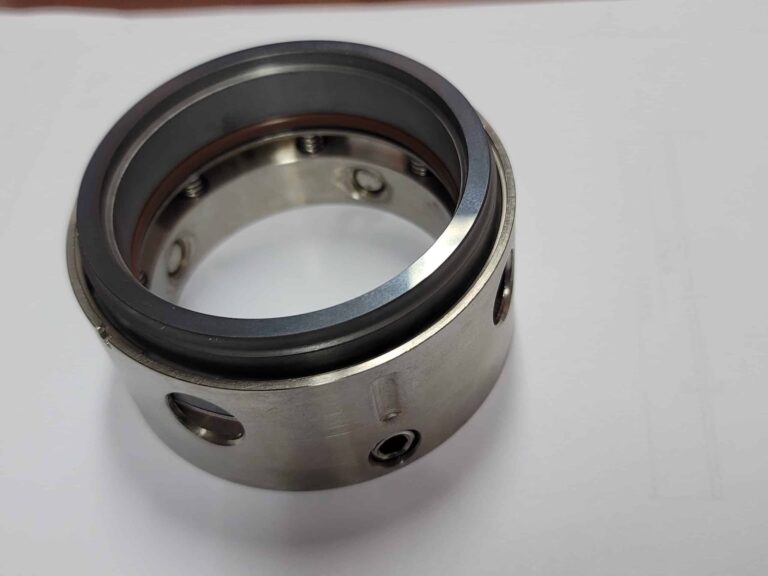
Seal faces specified to two helium light bands of flatness routinely deform to ten or more bands under dynamic conditions — a fluid film gap five times larger than the spec implies. The Poiseuille leakage formula itself takes thirty seconds, but the film thickness input you feed it determines whether your answer is off by 2x or by an order of magnitude.
The equation gives you a defensible leakage estimate only when you treat film thickness h as an engineering problem, not a textbook given. Every variable is measurable or available from the datasheet — except h.
The Poiseuille Leakage Equation and Its Variables
The standard leakage rate formula for flow between parallel seal faces is:
Q = (Delta-P x h^3 x b) / (12 x mu x L)
Where:
- Q = volumetric leakage rate (m^3/s)
- Delta-P = pressure differential across the seal faces (Pa)
- h = fluid film thickness between faces (m)
- b = face width in the circumferential direction, calculated as pi x mean face diameter (m)
- mu = dynamic viscosity of the sealed fluid (Pa-s)
- L = radial face width, the sealing length from ID to OD of the contact band (m)
This derives from Couette-Poiseuille flow in a thin annular gap under laminar conditions. The derivation assumes Newtonian fluid, constant gap height, and steady-state operation.
Three of these inputs come directly from the seal drawing and fluid data sheet. Pressure differential comes from process conditions. The one parameter you cannot pull from any document is film thickness h — and it sits in the numerator as a cube.
Double the pressure, double the leakage. Double the viscosity, halve the leakage.
But double h, and leakage increases eightfold.
How to Estimate Film Thickness h
Film thickness cannot be easily calculated, and it varies by orders of magnitude depending on seal design and operating conditions. In practice, h ranges from 5 to 50 microinches (0.13 to 1.27 um) across typical applications. Treating h as a single known value is the most common calculation error I encounter.
Film Thickness Ranges by Seal Type
Different seal designs produce fundamentally different film gaps. Use these typical industry ranges as starting points:
| Seal Type | Typical h Range | Application Context |
|---|---|---|
| Dry-running (gas seals) | 1 – 10 um | Non-contacting gas seals |
| Lubricated contacting | 0.13 – 1.3 um | Standard pump seals, most common |
| High-speed | 5 – 25 um | Hydrodynamic lift increases gap |
| Hydrostatic | 10 – 50 um | Externally pressurized, widest gap |
A standard cartridge seal on a centrifugal pump at 3600 RPM falls in the lubricated contacting range. Start at 0.5-1 um, then bracket with the full range to quantify sensitivity.
Why the Spec Sheet Underestimates h
Seal faces are specified to flatness within two helium light bands — approximately 23 microinches (0.58 um). That specification applies to static, unloaded faces on the inspection bench. Under operating conditions — thermal gradients, pressure deformation, shaft runout, vibration — deviations from flatness reach ten light bands or more.
A face that inspects at 0.6 um of flatness may operate with a 3 um effective gap once thermal distortion, chamber pressure effects, and dynamic loads take hold. Assuming the specification represents the operating condition is what makes leakage calculations unreliable.
What the spec sheet doesn’t tell you is that narrow face seals often leak less in practice despite the formula suggesting otherwise. Narrow faces resist thermal coning more effectively, producing a smaller actual gap. The formula says wider face = longer sealing path = less leakage, but gap geometry changes with face width in ways the parallel-plate model does not capture.
Worked Example with Sensitivity Check
Step-by-Step Calculation
Take a 50 mm mean diameter seal with a 5 mm radial face width, sealing ISO VG 32 oil at 10 bar differential pressure. Assume h = 3 um (an effective gap after thermal distortion, above the 0.13-1.3 um lubricated contacting range).
Parameters:
- Delta-P = 10 bar = 1,000,000 Pa
- h = 3 um = 3 x 10^-6 m
- b = pi x 0.050 = 0.157 m
- mu = 0.028 Pa-s (ISO VG 32 at 40 C)
- L = 0.005 m
Q = (1,000,000 x (3 x 10^-6)^3 x 0.157) / (12 x 0.028 x 0.005)
Q = (1,000,000 x 2.7 x 10^-17 x 0.157) / (0.00168)
Q approximately equals 2.5 x 10^-9 m^3/s, or about 0.15 cm^3/min.
That is roughly 0.15 mL per minute — about 180 drops per hour, far above the normal range for a properly installed seal.
What Happens When h Doubles
Recalculate with h = 6 um instead of 3 um — a modest increase from thermal distortion or face wear.
The cubic term changes from (3 x 10^-6)^3 = 2.7 x 10^-17 to (6 x 10^-6)^3 = 2.16 x 10^-16. That is an eightfold increase in calculated leakage from doubling one input. Reduce h from 5 um to 2 um, and leakage drops approximately fifteenfold.
A 50% error in your h estimate produces a 3.4x error in leakage prediction. A 2x error produces an 8x error.
This is why I always run the calculation at three h values — low end, midpoint, and high end for the seal type. If the range spans more than one order of magnitude, film thickness dominates your answer and you need better operating data before trusting any single number.
Acceptable Leakage Rates and Field Validation
Benchmarks
The widely accepted industry standard is 10 drops per hour or less per seal for standard pump applications. Many well-maintained seals operate well below this.
NGL pipeline pumps show field leakage from 50 mL/hr for isobutene at 200 psig to 3,000 mL/hr for ethane at 1,000 psig. These are primary-seal leakage rates from dual unpressurized seals on high-vapor-pressure services, not failures.
Comparing Calculated vs Measured Leakage
To validate your calculation, measure actual weepage at the drain port and compare. If calculated and measured values fall within the same order of magnitude, your h assumption is reasonable.
If the calculation predicts 0.1 mL/min but you measure 10 mL/min, your effective film thickness is roughly 4.6x larger than assumed — pointing to face distortion, misalignment, or vibration-induced separation.
API 682 defines leakage-detection plans (65A/65B, 66A/66B) for a reason: they provide a framework for distinguishing normal operation from developing failure. A seal trending from 2 drops/hour to 20 drops/hour over three months signals face wear — and your Poiseuille model, recalculated with updated h, can quantify that progression.
When the Poiseuille Model Breaks Down
The Poiseuille equation assumes laminar flow of a Newtonian fluid through a constant parallel gap at steady state. Each assumption fails in specific real-world conditions.
Non-Newtonian fluids — polymers, slurries, high-solids suspensions — break the linear viscosity relationship. I’ve seen an e-coat pump on an automotive paint line destroy cartridge seals every few months.
The tacky product migrated between faces during shutdown, creating adhesion that cracked the stationary seat ring on restart. The Poiseuille model had nothing useful to say because the fluid behavior bore no resemblance to Newtonian flow.
Vibration-induced face separation drives faces apart past the Reynolds film thickness, then slams them back into contact. This creates intermittent leak paths the steady-state formula misses entirely. Pumps near a critical speed or operating far from BEP are most vulnerable.
Two-phase flow occurs when sealed fluid flashes across the faces — common with light hydrocarbons or hot water near saturation. Once vapor forms in the gap, the single-phase viscosity assumption collapses.
Use the Poiseuille equation as a baseline for comparison, not a prediction with engineering certainty. When calculated and measured leakage diverge by more than 10x, stop refining h and start questioning whether the model applies at all.
Next Steps
Run the calculation at three film thickness values for your seal type, not one. The spread between high and low estimates tells you more than any single number — it quantifies how much your answer depends on the one parameter you cannot measure directly.
If the calculated range brackets your field measurement, your operating assumptions are sound. If it does not, the gap points to face distortion, environmental factors, or a fluid behavior the Poiseuille model was never designed to handle.