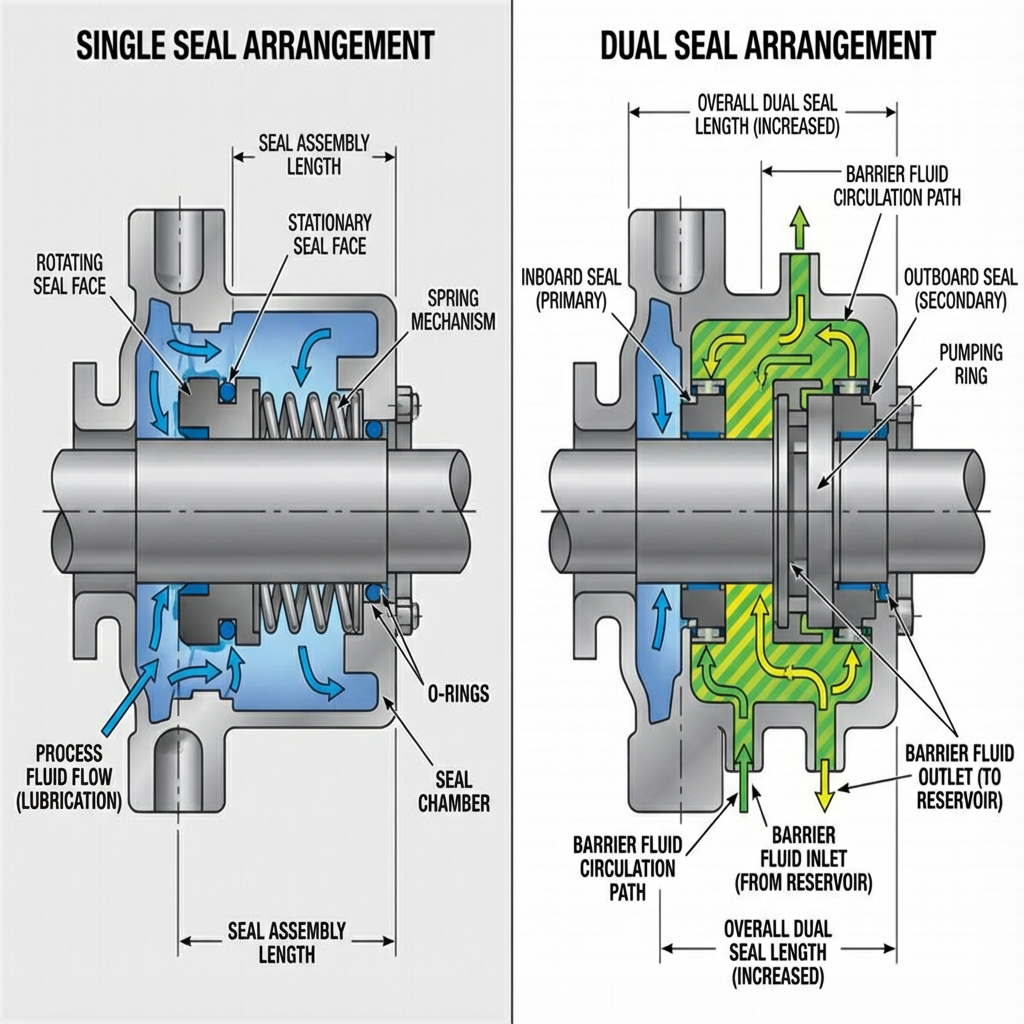
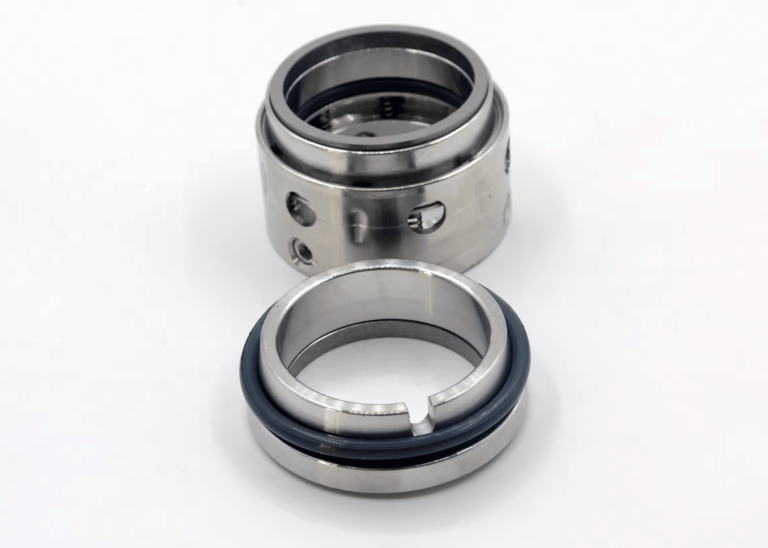
A mechanical seal material is the component substance that forms the sealing interface between a rotating shaft and its stationary housing — and the wrong specification is the root cause of most premature seal failures. This selection guide walks through the properties and property-limits that separate the four dominant face materials and the secondary-seal and hardware decisions that often silently cap the system’s real operating envelope. The face-pair selection logic — which materials run against each other under which conditions, and why hard-on-hard vs hard-on-soft pairings fail differently — lives on the dedicated face material combinations guide.
Every mechanical seal failure I investigate starts with the same question: was this the right material for the job? More often than not, the answer is no — not because the engineer picked the wrong category, but because the spec said “SiC” without specifying which SiC, or “carbon” without specifying which grade. Material names alone don’t prevent failures. Property numbers do.
Seal Face Materials
Four types of mechanical seal materials dominate face selection: carbon-graphite, silicon carbide, tungsten carbide, and alumina ceramic. Their properties overlap less than most catalogs suggest.
Carbon-Graphite Grades
Carbon-graphite is the default soft face material. Thermal conductivity runs 5-8 BTU/hr-ft-F — low compared to carbides, but carbon’s self-lubricating properties compensate by reducing friction-generated heat at the interface.
Not all carbon is the same. API 682 distinguishes two grades that matter:
- #9 Carbon (resin-filled): Rated to 500F. FDA-approved for food and pharmaceutical service. Adequate for general water and light hydrocarbon duty.
- #10 Carbon (antimony-filled): Rated to 700F. Blister-resistant because antimony fills the pore structure that would otherwise absorb process fluid under thermal stress. API 682 specifies this grade for refinery and chemical service.
That 200F difference is not academic. I’ve pulled carbon faces with raised circular blisters — small enough to miss on a visual check, large enough to separate the faces and cause leakage. Every one of those failures traced back to a resin-filled carbon running above its thermal limit.
Silicon Carbide Variants
Silicon carbide offers hardness at 9-9.5 Mohs (exceeded only by diamond, cubic boron nitride and boron carbide), thermal conductivity of 40-100 BTU/hr-ft-F, and temperature capability to 2550F in its raw form. But “SiC” on a purchase order is an incomplete specification. Three variants exist, and specifying the wrong one causes failures:
- Reaction-bonded SiC: Contains 8-12% free silicon. Adequate for neutral-pH applications, but the free silicon is chemically vulnerable — avoid pH above about 10, HF-bearing acids and hot concentrated sulfuric acid. I’ve seen reaction-bonded rings corrode in acid service that sintered SiC handles without issue.
- Direct sintered SiC: Pure SiC with full chemical resistance across the pH range. Costs more, but necessary for acid, caustic, or aggressive chemical service.
- Graphite-loaded SiC: Enhanced self-lubrication for dry-running or marginal-lubrication conditions. Trades some hardness for reduced friction in vapor and gas applications.
Tungsten Carbide
Tungsten carbide is the toughest face material — fracture toughness 3-5x higher than both SiC and alumina. Where SiC would crack under shaft deflection or mechanical shock, WC absorbs the impact. This makes WC the preferred choice for slurry pumps, mixers, and any application with vibration or misalignment.
Temperature rating is 750F as a solid ring, dropping to 500-700F when pressed into a metal holder. Density is 15.63 g/cm3 versus 3.1 g/cm3 for SiC — roughly five times heavier, which creates centrifugal loading on seal springs at high speeds.
Alumina (Ceramic)
Alumina ceramic is a legacy material for most new installations. Temperature limit sits below 350F, and thermal conductivity is poor compared to carbides, making alumina faces prone to heat checking — radial cracks from the ring center when thermal gradients exceed the material’s shock tolerance. Those cracks create cutting edges that destroy the mating face.
With SiC prices declining, the cost advantage that justified alumina has narrowed while the performance gap remains wide. For any application above moderate pressure, temperature, or speed, specify SiC or WC instead.
Face Pairing Logic
Face pairing follows one principle: one soft wearing face against one hard counter-face. Carbon-graphite against SiC is the most common tribological pair — carbon’s self-lubrication reduces friction while SiC’s hardness and conductivity handle heat dissipation.
The coefficient of friction between seal faces ranges from 0.03 to 0.3 — a 10x variation driven by material pair, process fluid, face load, and distortion. That range proves pairing is not arbitrary; it directly controls heat generation and wear rate.
For abrasive or high-particulate applications, dual hard faces (SiC vs SiC) are required because carbon erodes rapidly against suspended solids. In high-temperature service, WC vs WC provides the fracture toughness needed to survive thermal cycling. Avoid alumina against alumina — both faces are brittle, and any thermal shock causes cascading damage to both rings.
Secondary Seal Materials
Secondary seals fail more often from chemical attack than from wear. Selecting the wrong elastomer leads to swelling that locks up the seal or degradation that corrodes metal components. The right choice depends on temperature and pH together.
| Material | Temp Range | pH Range | Best For |
|---|---|---|---|
| NBR | -30 to +120C | 5-8 | Water, petroleum (neutral pH only) |
| EPDM | -40 to +140C | 6-14 | Steam, hot water, alkaline service |
| FKM (Viton) | -30 to +200C | 0-8 | Hydrocarbons, acids, high-temp oil |
| FFKM | -20 to +310C | 0-14 | Universal chemical resistance |
| PTFE | -250 to +260C | Full range | Cryogenic to high-temp, chemically inert |
FFKM at pH 0-14 is the only elastomer for mixed-chemical or unknown-fluid service. PTFE is not an elastomer — it seals by deformation rather than compression (Shore 55D versus 75A for FFKM), and requires different gland design to compensate for its lack of elastic memory.
For most hydrocarbon applications, FKM covers the operating envelope at reasonable cost. Reserve FFKM for aggressive chemical duty where FKM’s pH limit of 8 is insufficient.
Hardware and Wetted Metal Selection
Standard wetted metal is 316 stainless steel. Duplex stainless replaces it for sour service and high-chloride environments. Hastelloy-C, Inconel 718, or Alloy-20 serve aggressive chemical and high-temperature applications.
API 682 Type B and C seals mandate Hastelloy-C or Inconel 718 for bellows — not optional for refinery service.
The hardware choice most engineers overlook is the face insert holder. What the spec sheet doesn’t tell you: a solid SiC ring reaches 800F, but press it into a 316SS holder and the assembly’s temperature rating drops to as low as 200F. The holder becomes the thermal bottleneck.
For high-temperature duty, Invar or Alloy-42 holders preserve the face material’s capability; standard 316SS holders cut it by 75% or more.
What Real Service Does to Published Ratings
Every material property above comes with a lab-condition asterisk. Real pumps introduce complications that shift the failure mode from “material limit” to “specification error.”
A pump running at pH 11 on reaction-bonded SiC won’t fail immediately — it corrodes gradually as the free silicon reacts, losing surface finish until leakage climbs. The failure report says “seal face degradation” instead of “wrong SiC variant.” A #9 carbon in hot service develops blisters so slowly the operator attributes rising leakage to normal wear. The API 682 standard specifies #10 carbon for thermal service precisely because this failure mode is invisible until the seal is pulled.
Temperature ratings mislead the most. An 800F SiC face in a 316SS holder operates at a 200F ceiling — the holder, not the face, was the weakest link all along.
Three specification checks prevent more failures than any material upgrade: specify the variant (not just the category), confirm the holder material, and match elastomer pH range to actual process chemistry.
Cost-Per-Running-Hour: When Premium Faces Pay for Themselves
Procurement decisions made on purchase price alone keep losing money. A standard carbon-graphite face runs roughly one-quarter to one-third the price of silicon carbide; alumina sits at 1.2–1.5x carbon; tungsten carbide and silicon carbide both fall in the 2–4x range, and the gap between TC and SiC is usually smaller than the gap between carbon and the hard-face group. The economics shift sharply once you account for what happens after the line item: re-lapping potential, failure frequency, and what a single unplanned shutdown costs the line.
Hard faces (SiC, TC) can be re-lapped multiple times — a single SiC face rebuilt three times spreads its purchase price across four service cycles, dropping per-use cost well below sticker. Carbon graphite is typically single-use; once worn past tolerance, it is scrapped. Labor cost per change-out is identical regardless of face material, so a cheaper face that fails twice as often doubles your labor without saving anything material. In one chemical-plant audit, a pump was burning $10K/month in seal replacements but driving $20K/month in product loss and 15 hours of unscheduled downtime — purchase price was 28% of the actual monthly failure cost.
Map face material to severity tier, not to standardization preference:
- Mild service (clean water, moderate temperature, no abrasives): carbon-graphite delivers full rated life. Upgrading to SiC adds cost without reducing failures — the crossover never arrives.
- Moderate service (light chemical, occasional particulate): carbon still works but service intervals shorten. TC or SiC extends MTBF and opens the re-lapping option. If you are replacing carbon faces more than once a year on a given pump, run the TCO math — crossover typically lands within 18–24 months.
- Severe service (high temperature, abrasive slurry, aggressive chemicals): carbon fails fast and often. Sintered SiC variants (not reaction-bonded, which aggressive chemicals attack) are not premium choices — they are the only choices that keep total cost down.
The hidden cost most buyers miss is the assumption that every pump needs the same face material. Calculate cost-per-running-hour for each pump, not cost-per-unit at purchase, and material selection stops being a procurement argument and becomes an engineering decision.
Specifying Material Without the Common Failure Patterns
SiC is not one material. Carbon is not one grade. Your seal’s temperature limit is often set by the holder, not the face.
Start every material specification with these three questions:
- What is the process fluid pH? Caustic conditions (pH above about 10), HF-bearing acids or hot concentrated sulfuric acid eliminate reaction-bonded SiC
- What is the maximum operating temperature including upsets? The holder material — not the face — usually caps thermal capacity, and EPDM secondary seals limit even SSiC faces to roughly 140 °C
- Is there abrasive particulate? Hard-on-hard pairings (SSiC vs SSiC, WC vs WC) become mandatory once suspended solids enter the process stream
The answers narrow your face material, face pairing, secondary seal, and hardware selection to one or two viable options — then confirm every component in the assembly can handle the conditions independently.