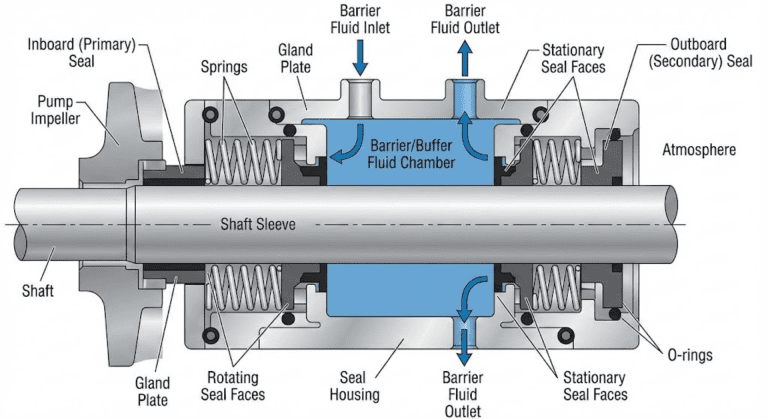
Pull a conventional pusher seal out of a pump, then pull a bellows seal out of another. The pusher has a visible coil spring pushing against a slider that rides on the shaft with an O-ring behind it. The bellows has neither — just a corrugated sleeve (metal or rubber) anchored at one end and bonded to the rotating face at the other.
The parts look different because the bellows is doing two jobs at once. It is simultaneously the secondary seal and the spring, one integrated component replacing the coil-spring-plus-dynamic-O-ring pair you are used to seeing inside a mechanical seal. Understand that single substitution, and everything else about bellows selection follows.
The Dual-Function Part Inside a Bellows Seal
The bellows does two things simultaneously. It flexes axially like a spring, keeping the rotating face pressed against the stationary face as the faces wear. It also seals between the rotating face and the shaft sleeve, doing the job that a separate dynamic O-ring does in a pusher design.
One corrugated element, two functions, zero sliding parts behind the face. Descriptions that frame the bellows as merely “spring-style” or as “removing the elastomer” each capture only half the picture, and you cannot troubleshoot a bellows seal correctly holding just one half.
The Shop-Floor Symptom That Proves It
Here is the symptom that makes the dual role concrete. In a pusher seal running certain refrigerants or hydrocarbons, Buna-N gasket swelling is a visible warning of imminent failure — the dynamic O-ring is losing to the process fluid. Jeremy Marwil of CH2M HILL documented this in Plant Services as a tell-tale cue maintenance teams learn to spot.
A bellows seal cannot fail that way. There is no Buna-N O-ring on the shaft to swell, because the bellows itself is handling that sealing job in a stationary-to-rotating-face path instead of a sliding-elastomer path. You trade that failure mode for a different one (fatigue in the convolutions), but the chemical-compatibility vulnerability is gone.
The Reframing That Changes Troubleshooting
The most common mistake I see is technicians treating a bellows seal like a spring seal with a fancy spring. It is not. The corrugated sleeve is also a gasket — and that reframing changes how you install it, how you diagnose failures, and how you spec a replacement.
What Bellows Construction Replaces
Spring-Plus-O-Ring Collapsed Into One Part
A bellows replaces the entire spring-plus-dynamic-O-ring subassembly of a pusher seal — not just the coil spring designs you see in a Type 21 or API Plan 01 layout. In a conventional pusher mechanical seal, the spring generates closing force on the face while a separate elastomer O-ring slides axially on the shaft or sleeve. Two parts, two functions — bellows collapses both into one.
The Temperature Envelope Shift
The substitution changes the temperature envelope immediately. The pusher design is capped by its elastomer, not by its metallurgy.
Industry practice typically puts pusher-seal elastomer secondary seals near 150°C, and even FFKM — the most temperature-capable elastomer on the market — is typically rated to around 325°C continuous service. Above that, the O-ring is disqualified, and any seal that relies on a sliding elastomer is disqualified with it. The bellows architecture does not have that ceiling because it has no sliding elastomer to lose.
The Fatigue-Life Trade-Off
The trade-off appears in a different place. Bellows are fatigue elements — each pressure, thermal, or displacement cycle loads the convolutions, and bellows have a finite cycle life. The valve industry designs bellows for roughly 100,000 cycles as a working convention.
That is a real constraint, but not the same constraint as elastomer temperature disqualification. Which failure mode you prefer depends on your service. The full comparison between pusher and bellow seals covers the trade-off in depth.
The decision is not “which seal lasts longer” — it is “which failure mode is acceptable in this service.”
The Two Problems Bellows Construction Solves
Bellows construction eliminates two distinct failure modes that plague pusher seals: shaft hang-up and elastomer disqualification. These are the reasons a pump gets specified with a bellows in the first place.
Shaft Hang-Up
Hang-up happens when the dynamic O-ring in a pusher seal cannot slide. In normal operation, the O-ring must move axially along the shaft as the face wears, keeping the spring-loaded face in contact with the stationary face.
If the shaft surface frets, the process fluid crystallizes on the atmospheric side, or corrosion roughens the sleeve, the O-ring catches and stops moving. The spring cannot follow the face wear because the O-ring is holding the face assembly back. Face contact breaks, leakage starts, and the seal fails — often with the spring still at full rated force, uselessly.
Product solidification is one of the more stubborn hang-up causes, particularly on the atmospheric side of the seal where temperature drops and materials crystallize out. A bellows seal has no sliding element on the shaft — the corrugated sleeve flexes axially instead of sliding, so fretting and crystallization have nothing to grab. This is the single biggest reason bellows are specified where the pump sees shaft surface wear over time.
Elastomer Disqualification
The second problem is chemical or thermal. Above roughly 150°C in standard service (260°C with fluorocarbon, 325°C with FFKM), the elastomer O-ring fails — it hardens, swells, extrudes, or degrades. Aggressive process chemistry does the same thing at lower temperatures.
Once the elastomer is disqualified, the pusher architecture has no fallback, because the dynamic sealing path requires a sliding gasket. A bellows seal moves the secondary sealing function into a metal (or rubber, or PTFE) corrugated sleeve that does not rely on sliding-elastomer compliance at all.
I pulled a 316L stainless bellows from a brine pump last year that had corroded through in 72 hours — chloride attack at elevated temperature. The lesson was not “bellows failed.” The lesson was that bellows material selection is a separate decision from bellows-vs-pusher architecture selection.
The architecture was correct — an elastomer O-ring would have failed faster. The material was wrong for the chloride concentration.
Switching to Hastelloy C-276 and correcting a 0.005″ shaft misalignment brought unplanned downtime down by about 40%. Architecture first, material second — in that order.
Bellows themselves come in three material families — elastomer, metal, and PTFE — and the choice between them is a separate decision.
When Bellows-Style Construction Is Required
Bellows-style is required, not optional, in three service conditions: high-temperature above the elastomer ceiling, cryogenic where elastomers lose flexibility, and shaft-fretting service where pusher hang-up is recurring. Outside those, a pusher seal is cheaper, simpler, and perfectly adequate.
API 682 Type A, B, and C
API Standard 682 codifies the high-temperature cutoff in its Type A/B/C classification. Type A is the conventional O-ring pusher seal.
Type B is a metal bellows seal that still uses a static elastomer O-ring as the gland-side secondary seal. Type C replaces even that static O-ring with flexible graphite, for services where no elastomer is acceptable anywhere in the seal envelope.
The Type B to Type C step is the industry’s formal answer to “when is even a static elastomer disqualified.” It is a useful anchor when you read seal spec sheets — knowing whether your service is a Type B or Type C tells you more than a temperature number alone.

Temperature and Pressure Envelopes
Metal bellows seals reach published ceilings of 425°C (800°F) in standard product lines, with edge-welded constructions pushing above 1500°F (815°C) in specialty service. API 682 Category 2 covers the API-610 pump envelope at −40 to 399°C and pressures up to 42 bar, which brackets most refinery and petrochemical bellows applications.
Cryogenic service — liquid nitrogen, LNG, liquid oxygen — sits at the other end of the same disqualification. Elastomers lose pliability at low temperatures and either leak or hang up, while 347 SS bellows cores maintain strength without becoming brittle.
Routing to the Right Bellows Family
Standard-duty pumps running ambient or moderate-temperature water, clean chemicals, or general process fluids do not need bellows construction. Elastomer bellows like Type 1 and Type 21 handle these services.
When service conditions rule out elastomer entirely, metal bellows mechanical seals are where that decision leads. For readers already committed to welded metal and needing to specify diaphragm count, material, and geometry, welded metal bellows selection covers the next-step detail.
How the Bellows Behaves Mechanically
Bellows are not drop-in springs — their behavior follows rules coil springs do not. Three engineering facts are worth knowing if you ever have to troubleshoot or spec one.
The Bellows Settles
The length you receive from the factory is not the length the bellows runs at. Free length stabilizes at roughly 15 to 25% of as-welded length after initial cycling — so a new bellows will appear longer than the service-worn one you pulled out, and that is normal, not a manufacturing defect.
Compression Is Safe, Extension Is Not
Bellows should work mostly in compression, with 20% extension maximum. Extension fatigues the convolutions asymmetrically — weld roots and diaphragm inner diameters see higher cyclic stress on the pull stroke than the push stroke.
If you install a bellows with the face too far out and the spring element has to extend to reach contact, you have halved its cycle life before the pump is even commissioned.
Spring Rate Is Hypersensitive to Thickness
A ±5% change in diaphragm material thickness produces a ±10% change in spring rate. Face-closing force — and therefore face wear rate, heat generation, and seal life — depends on manufacturing tolerances you cannot see from the outside.
This is why bellows count and construction quality matter in a way spring count does not. Some manufacturers run more convolutions than the industry-standard eight specifically to reduce per-convolution stress and extend fatigue life.
The Bellows Decision in One Paragraph
Here is the framework for routing your own selection. If your service is standard-duty pump water or compatible chemicals at ambient to moderate temperature (below ~150°C), an elastomer bellows in the Type 1 or Type 21 family is adequate — and a pusher seal will work just as well, so the choice is economics.
If you exceed the elastomer temperature limit, hit chemistry the O-ring cannot survive, or work in cryogenic service where the elastomer hangs up, metal bellows is required, not optional — and you are choosing between edge-welded and formed construction from there.
If your pump shows recurring hang-up from shaft fretting or product solidification regardless of temperature, any bellows architecture eliminates that failure mode by removing the sliding element. Before you spec, check which of the three conditions you actually have. The wrong answer costs you a premature teardown; the right answer buys you the seal life the architecture is designed to deliver.